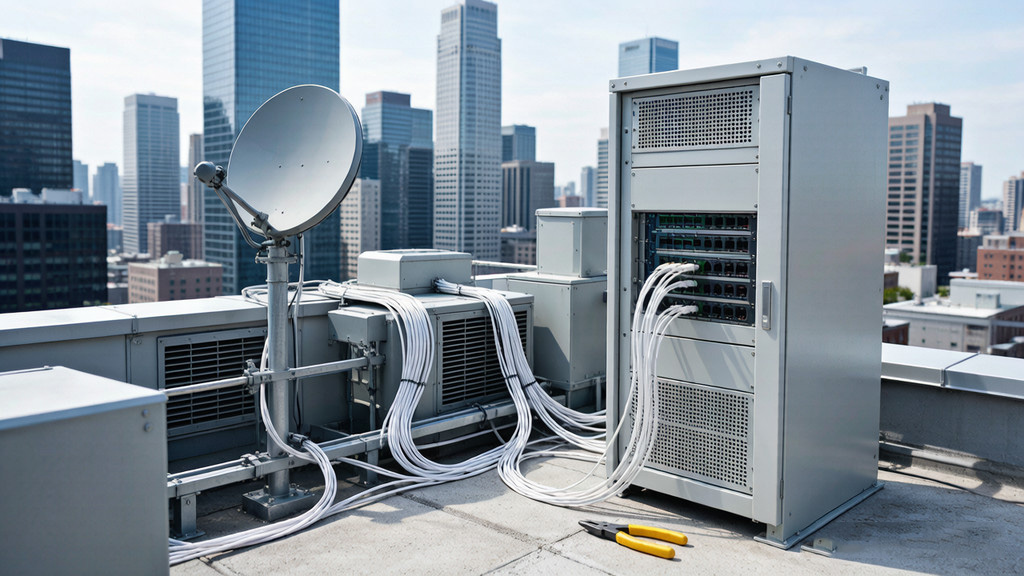
MasOrange, Vodafone Spain and GIC have signed an agreement to create an innovative fiber optic company (FiberCo) in Spain. Spain's largest fibre optic network is coming, as MasOrange, Vodafone Spain, and GIC team up in a €5 billion joint venture to boost digital infrastructure and sustainability across the country. Customers from both operators will be able to use this FTTH (fibre-to-the-home) network. MasOrange to hold a 58% stake in the co-controlled FiberCo joint venture with Vodafone Spain and. Spain's fixed broadband market took another significant step toward consolidation this week, with MasOrange and Vodafone Spain – now owned by UK-based investment firm Zegona – announcing the creation of the country's largest fibre network company in partnership with Singapore's sovereign wealth. Zegona Communications has confirmed a significant new partnership between Vodafone Spain, MasOrange, and global investor, GIC Private Markets, to establish FibreCo, a nationwide fiber network operator in Spain. (“MasOrange”) (together the “Parties”) have signed a confidential non-binding term sheet setting out the proposed key terms for a national network sharing agreement.
[PDF Version]
Cold joints occur when a fresh concrete batch is poured against a partially hardened existing layer. As you know, concrete hardens through chemical reactions between cement aggregate, water, and air. This discontinuity occurs because the older material has passed its initial setting time, preventing a true chemical bond with the fresh mix. The full knitting together of the two batches of concrete under vibration to form a homogeneous. Based on the structural characteristics of the belt conveyor, laser ranging technology, and GNSS-RTK positioning technology, an algorithm is proposed to determine the operating status of the belt conveyor, calculate the position and area of the mixed material, and record the pouring and compaction. Explore the full spectrum of services and industries covered by B. Few defects pose a more immediate and. ACI Committees, Membership, and Staff have answered common questions on a variety of concrete related topics. What is the difference between a contraction joint, isolation joint, expansion joint, construction joint, and a cold joint? A.
[PDF Version]
The bend radius of fiber cables is critical for maintaining high performance and longevity. During installation under tension, maintain a minimum bend radius of 20 times the cable's outer diameter, while post-installation requires a minimum long-term bend radius of 10 times the. Fiber optic cable bend radius is a critical mechanical parameter that determines how sharply a cable can be bent without risking microbending, macrobending, signal loss, or long-term structural fatigue. It is measured from the inside of the bend, not the outer curve. Installers must understand these specifications and know how to install cables without. Fiber optic cables are designed to withstand some bending, but excessive bends can physically damage the glass fiber or cause significant signal loss.
Explore cut-to-size twinwall polycarbonate sheets for hot and cold aisle containment in data centers. Lightweight, impact-resistant, and flame-rated materials that improve cooling efficiency and reduce energy costs. Armstrong aisle containment combines flexible design, strategic sourcing, and American manufacturing to deliver solutions that ensure long-term performance in a rapidly evolving digital world. The Sliding Doors reduce data center. While liquid cooling is critical for managing extreme rack densities, hot aisle containment (HAC) systems capture and isolate hot exhaust air, and cold aisle containment (CAC) systems enclose and direct cold supply air. Both approaches remain essential since most high-density environments still mix. Traditional open aisle data centres use perimeter PAC (precision air conditioning) or CRAC (computer room air conditioning) units to channel cold air up through a raised floor void via grilles positioned in front of the IT cabinets.
[PDF Version]
In fusion splicing, the ends of the fibers are welded together with heat. With mechanical splicing, the fibers are positioned in a self-contained unit where adhesive or a mechanical device holds. When installing a fiber optic network, connectors are required to connect both ends of the fiber optic cable. Common splicing methods include optical fiber cold splicing and optical cable hot fusion splicing. Both techniques have their advantages and are suited for different applications, but understanding which method to use can greatly impact the network's. This is where fiber optic cable splicing—the process of creating a permanent, high-performance join between two fiber ends—becomes critical. For network managers and technicians, a poor splice can lead to significant signal degradation, network downtime, and costly troubleshooting. - Process: The fibres are precisely aligned using a fusion splicing machine, and a controlled arc or laser heat source is applied to melt the fibres. The cold cure method, also known as mechanical splicing, involves the combination of anaerobic adhesive and activator.
[PDF Version]
A critical aspect around battery pack busbars are the joints. It is important to consider the fundamental requirements of the joint: In reality the connecting surfaces are not perfectly flat. The surface roughness will effectively reduce the actual electrical contact. Preventing hot joints requires three elements executed correctly: proper surface preparation (removing oxidation and achieving metal-to-metal contact), correct torque application (creating sufficient contact pressure without damaging threads), and ongoing thermal monitoring (catching deterioration. The IEC standard for busbar contact resistance plays a vital role in ensuring electrical safety, performance, and longevity of electrical systems. In power distribution networks, busbars are essential components that carry large amounts of current. The surface roughness will effectively reduce the actual electrical contact area., the overlap length no longer needs to match the width.
[PDF Version]
Adhesive (Butt & Wrap) Joints: Fiberglass tape and epoxy adhesive create a monolithic, leak-proof joint. These butt-and-wrap joints cure to full strength, becoming “as strong as the pipe itself”. They are ideal for high-pressure or permanent installations, and they eliminate metal. FRP Butt Joint Fiberglass Kit is a package of fiberglass strips precut for FRP technician on the field or shop as ready use Fiberglass reinforcement to fabricate Butt Joint FRP Pipes and Fittings lamination without going through time consumed preparation of cutting different types and sizes of. This quick guide demonstrates how to perform butt joints using OTA Fiberglass Pipe Tools. no matter the type of pipe/its origin, this easy-to-follow tutorial as well as the. FRP SYSTEMS offers a complete line of standard and custom made fittings. Elbows, laterals, tees, reducers, full face flanges, vanstone flanges and blanks are readily available for shipment from stock. This type of joint compound comes in a powder form and with different setting times like 20 minute, 45 minute or 90 minute.
[PDF Version]
This paper is focused on hybrid busbar joints with a twofold objective of understanding the differences in electrical resistance under service conditions and evaluating their performance when subjecte.
Perform a visual inspection of the optical fiber cable line to look for any visible signs of damage or abnormalities. Effective maintenance of cable intermediate joints requires a structured approach combining visual inspection, electrical testing, and preventive care protocols. The inspection process involves multiple stages, from initial visual assessment to advanced diagnostic testing, each designed to identify. This document outlines the Panduit recommended procedures for visual inspection and cleaning of multimode and singlemode structured cabling system interconnect components (connectors and adapters) and specifies workmanship requirements, tools and best practices, to be utilized for end face. For every fiber optic cable plant, you need to test for continuity and polarity, end-to-end insertion loss and then troubleshoot any problems.
Contact us for competitive quotes on any of our power communication and smart grid products
Get a Quote